The MOLLE grid is laser-cut into a welded outer panel rather than stitched as webbing rows, so the waterproof barrier behind it remains continuous. Retention straps are positioned to secure the fore-end, receiver and stock independently, and strap count and position are set against a customer reference firearm. Body length is quoted at 132 cm with 122 cm and 140 cm also available.
Foam is graded by position rather than applied at one thickness: 20–25 mm profiled egg-crate in the lid, 15 mm in the base and 10 mm at the sides. The lid profile compresses progressively and presses the firearm against the base, so the gun is held between two foam surfaces rather than resting under a flat lid.
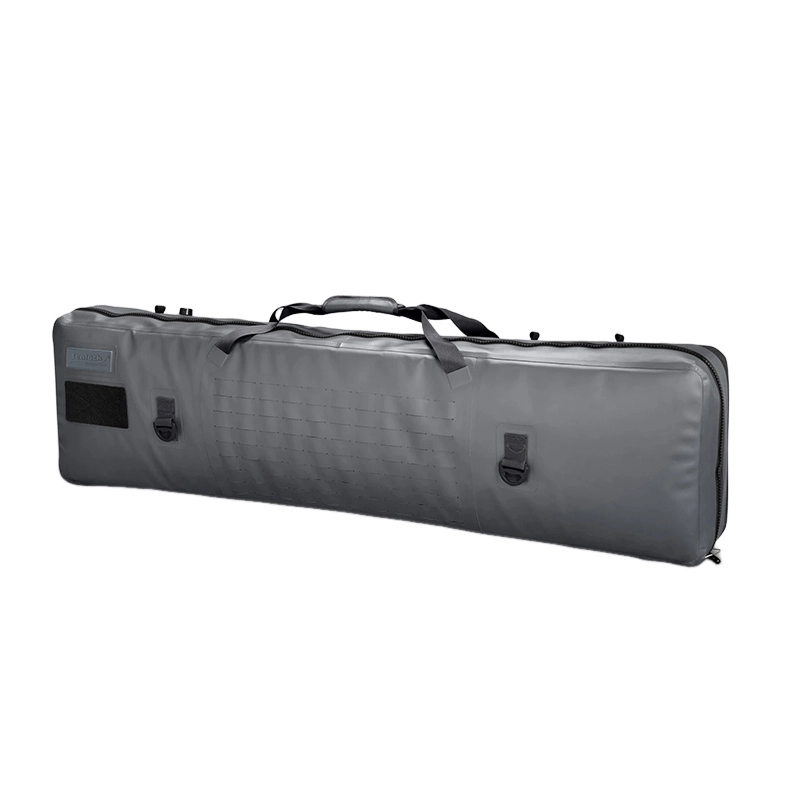
SL-C811 in grey, showing laser-cut MOLLE, D-rings, hook-and-loop panel, and full-length waterproof zipper
| Specification | Value |
| Model | SL-C811 |
| External size | 132 × 33 × 10 cm (estimated) |
| Capacity | approx. 42 L |
| Weight | approx. 2.6 kg (estimated) |
| Shell material | 840D TPU laminated fabric |
| Construction | RF welded |
| Waterproof rating | IPX6 |
| Closure | Full-length two-way waterproof zipper |
| Padding | EVA foam, 20–25 mm |
| Internal retention | Adjustable fixing straps |
| Exterior system | Laser-cut MOLLE, D-rings, hook-and-loop panel |
| Carry | Backpack straps, detachable shoulder strap, reinforced handle |
| Colourways | Grey / Brown / Camouflage |
| MOQ / Sampling / Production | 300 pcs / 7–10 days / 30–45 days |
Dimensions and weight are stated as estimated against the current production sample and are confirmed on the approved sample for each order.
| Requirement | What Usually Gives Way | How the SL-C811 Keeps It |
| Waterproofing | Stitched MOLLE and padding perforate the shell | Welded shell; MOLLE laser-cut into a welded panel |
| Impact protection | Welded dry cases run unpadded to save weight | 20–25 mm EVA egg-crate upper, 15 mm base, 10 mm sides |
| Exterior load carriage | Sewn webbing rows pierce the barrier | Laser-cut MOLLE on a welded outer panel |
| Internal security | Foam alone lets a firearm shift | Adjustable retention straps at multiple points |
| Carry over distance | Handles only, or thin single straps | Backpack harness plus detachable sling |
The cost of holding all three is weight. At approximately 2.6 kg this is the heaviest case in our range, and it should be specified where the protection and load carriage are needed rather than as a general-purpose product.
The interior is the reason this case exists. A welded shell keeps water out; the retention system and layered foam are what keep the firearm undamaged inside it.
Interior: egg-crate upper foam, adjustable retention straps, and padded base
The lid carries a profiled egg-crate foam layer at 20–25 mm. The profile does two things a flat sheet does not: it compresses progressively rather than all at once, and its raised sections press down onto the firearm to hold it against the base rather than simply covering it. When the case is closed the gun is held between two foam surfaces rather than resting loose under a lid.
Multiple adjustable fixing straps run across the base, positioned so a rifle can be secured at the fore-end, the receiver, and the stock independently.
• Six to eight adjustable retention points across the length
• Positioned to secure fore-end, receiver, and stock separately
• Adjustable rather than fixed, so a shorter or longer firearm is held equally
• Secured so a scoped rifle with a suppressor fitted stays in position rather than travelling
Retention is what separates a tactical case from a padded bag. Padding absorbs an impact that reaches the firearm; retention stops the firearm moving in the first place, which is the mechanism that produces contact wear on long journeys.
| Position | Thickness | Function |
| Upper lid | 20–25 mm EVA egg-crate | Compresses progressively; presses the firearm to the base |
| Base | 15 mm EVA | Takes ground contact and drop energy |
| Sides | 10 mm EVA | Protects against edge impact and case-wall contact |
Foam is graded by position rather than applied at one thickness throughout. The base takes the heaviest loads, the lid does the retention work, and the sides need enough to stop edge contact without adding unnecessary bulk to a 10 cm profile.
Conventional MOLLE is rows of webbing stitched to a panel. On a waterproof case that is hundreds of needle holes across the largest face of the product, which is why most welded cases carry no MOLLE at all.
How ours is done. The MOLLE grid is laser-cut into a welded outer panel. There is no webbing and no stitching — the attachment slots are openings in a panel that is itself welded to the shell, so the waterproof barrier behind it is continuous.
What it accepts. Standard MOLLE and PALS-compatible pouches and accessories, plus two D-rings for lash points and a hook-and-loop panel for identification or unit patches.
Why laser cutting rather than punching. A laser-cut edge is sealed as it is cut, so the slot edges do not fray or delaminate under repeated attachment and removal.
| Worth checking on any waterproof tactical case:ask whether the MOLLE is stitched or laser-cut. Stitched webbing on a welded shell is common, and it puts a perforation at every bar-tack across the case's largest panel. Ask for the immersion test to be run on a finished unit with the MOLLE panel fitted rather than on a bare shell. |
Brown colourway
| Element | Detail |
| Full-length waterproof zipper | Two-way, so the case can be opened from either end or partly opened |
| Backpack straps | Adjustable; distribute a 2.6 kg case plus firearm across both shoulders |
| Shoulder strap | Detachable, for single-shoulder carry and short transfers |
| Carry handle | Reinforced, centre-mounted for balanced lifting |
| D-rings | Two, for lashing or accessory attachment |
| Hook-and-loop panel | Identification, unit, or brand patches |
| MOLLE grid | Laser-cut, PALS compatible |
The two-way zipper matters more on a case this long than on a short one. Opening from the muzzle end alone gives access to the barrel section without exposing the whole interior, which is useful when working from a vehicle or a prone position.
The shell is 840D TPU laminated fabric joined by RF welding, so there are no stitch perforations in the waterproof body. The closure is a full-length waterproof zipper, and the MOLLE panel is laser-cut rather than sewn.
| Element | Contribution |
| 840D TPU laminated shell | Non-porous barrier; abrasion resistant |
| RF welded seams | No needle perforations in the body |
| Waterproof zipper | Seals the opening rather than merely closing it |
| Laser-cut MOLLE panel | Load carriage without piercing the barrier |
| Welded strap anchors | Carry load transferred without stitching through the shell |
| Rated IPX6:protection against powerful water jets from any direction under IEC 60529 — heavy rain, deck wash, and hose-down. It is not rated for immersion. A padded tactical case of this construction is specified for weather and transport protection, and customers whose cases may go fully underwater should be directed to our welded roll-top range, which is immersion rated and floats. | |
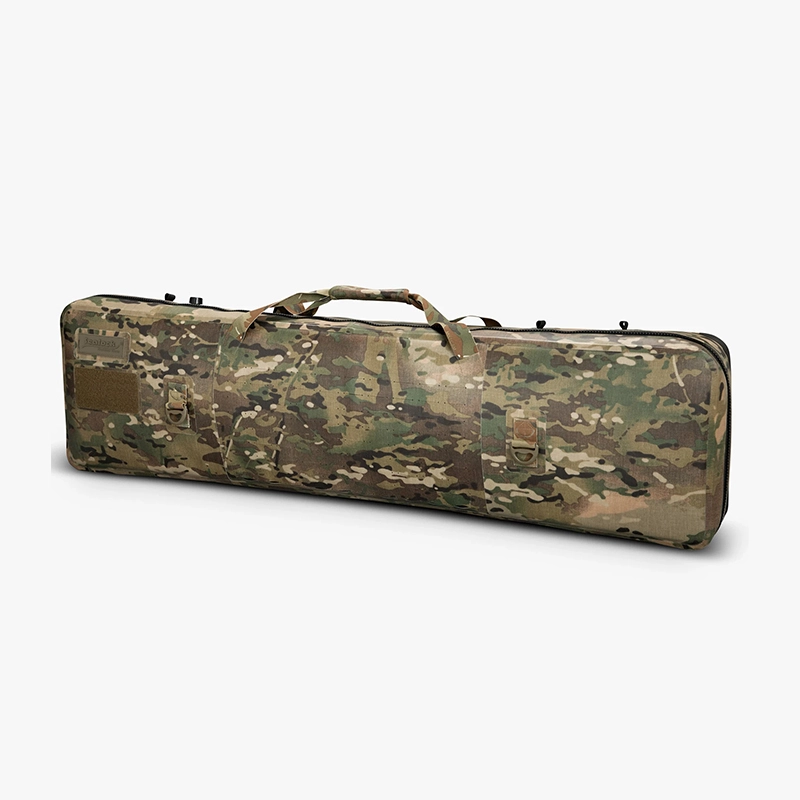
Camouflage colourway
| Colourway | Typical Use |
| Grey | Range, agency, and low-profile transport |
| Brown | General field and tactical use |
| Camouflage | Hunting and concealment applications |
Custom colors and camouflage patterns can be matched for OEM programmers, and the hook-and-loop panel accepts identification patches without additional branding on the shell.
| Item | Specification |
| Model | SL-C811 |
| Product name | Tactical Waterproof Rifle Case |
| Product type | Tactical long gun case |
| External size | 132 × 33 × 10 cm (estimated) |
| Capacity | approx. 42 L |
| Weight | approx. 2.6 kg (estimated) |
| Shell material | 840D TPU laminated fabric |
| Inner lining | Polyester |
| Foam | EVA |
| Foam thickness | 20–25 mm upper / 15 mm base / 10 mm sides |
| Construction | RF welded |
| Waterproof rating | IPX6 |
| Closure | Full-length two-way waterproof zipper |
| Internal retention | Adjustable fixing straps, 6–8 points |
| MOLLE system | Laser-cut, PALS compatible |
| Accessory mounts | 2 D-rings, hook-and-loop panel |
| Backpack straps | Adjustable |
| Shoulder strap | Detachable |
| Carry handle | Reinforced |
| Compatible firearms | Precision, tactical, hunting, scoped, and AR-style rifles; shotguns |
| Colourways | Grey / Brown / Camouflage |
| MOQ | 300 pcs |
| Sample lead time | 7–10 days |
| Production lead time | 30–45 days |
| OEM / ODM | Supported |
| Origin | China |
| Option | Notes |
| Body length | 132 cm standard; 122 cm and 140 cm quoted |
| Foam thickness and grade | Adjusts protection level and case weight |
| Retention strap count and position | Set against a reference firearm |
| MOLLE grid layout | Panel size and slot pattern |
| Hook-and-loop panel size and position | For unit or brand identification |
| Colour and camouflage | Pantone and pattern matching |
| Interior lining colour | Contrast lining for visibility of small parts |
| Welded logo patch | Applied without piercing the shell |
| Packaging | PE bag standard; retail carton and hang tag available |
At 132 cm external the case suits rifles up to roughly 120 cm overall, which covers scoped precision rifles with suppressors fitted — the configuration that most commonly runs out of room in a shorter case.
1. Measure the firearm overall as it will be cased, with optic, suppressor, and any bipod fitted
2. Allow clearance beyond that figure rather than specifying to the exact length
3. Confirm the retention strap positions suit the fore-end, receiver, and stock of that firearm
4. For AR-style rifles, confirm whether the case carries one rifle with accessories or two rifles
5. Send a reference firearm at sampling where the fit is critical
6. Incoming inspection of 840D TPU, EVA foam, lining, webbing, and zipper
7. Welding parameter setup for the fabric batch and first-article peel test
8. Precision cutting of shell panels, foam, and lining
9. Laser cutting of the MOLLE grid panel
10. RF welding of the shell body and MOLLE panel to the case
11. Waterproof zipper installation into the welded seam
12. EVA foam layering — egg-crate upper, base, and side sections
13. Retention strap installation and lining assembly
14. Backpack harness, shoulder strap, handle, and D-ring mounting
15. Water resistance and function verification
16. Final inspection and export packing
| Check | Method | Frequency |
| Incoming material | Visual and dimensional | Every batch |
| Weld peel test | Destructive peel on a sample weld | Start of every run |
| Welded seam integrity | Full visual inspection | 100% |
| MOLLE panel weld | Visual around the panel perimeter | 100% |
| Laser-cut slot edges | Inspection for clean sealed edges | 100% |
| Foam placement and thickness | Measured against specification | Sampling |
| Retention strap function | Adjustment and hold check | 100% |
| Zipper operation | Full-length two-way operation | 100% |
| Harness and handle | Loaded pull test | Sampling |
| Water resistance | Jet spray check against the IPX6 condition | Per approved sampling plan |
| Packaging | Carton verification | 100% |
| Test | Method | Outcome |
| IPX6 water jets | Powerful jets applied from multiple directions | No ingress at seams, closure, or MOLLE panel |
| Weld seam peel | Destructive peel on a welded sample | Parent fabric tore before seam separation |
| MOLLE panel immersion | Jet test with the laser-cut panel fitted | No ingress behind the panel |
| Retention hold | Loaded case handled and transported over rough ground | Firearm held position; no travel within the case |
| Drop with retention | Loaded case dropped onto the base | Foam and retention absorbed the impact; no contents damage |
| Foam recovery | Repeated compression of the egg-crate layer | Recovered; no permanent flattening |
| Harness load | Repeated loaded carry cycles on the backpack straps | No anchor separation or webbing deformation |
| Two-way zipper cycle | Repeated operation from both ends | Both sliders retained function and sealing |
| MOLLE attachment cycle | Pouches repeatedly attached and removed | Slot edges intact; no fraying or delamination |
| Abrasion | Contact with vehicle beds, gravel, and hard surfaces | Cosmetic wear only; barrier intact |
| Model | Construction | Rating | Weight | Padding | Chosen For |
| SL-E899 | Stitched, coil zip | Water-resistant | 0.85 kg | 10–15 mm | Everyday field and range |
| SL-E603 | Welded, sealed zip | IPX7 | 1.1 kg | None | Waterproof with fast access |
| SL-E302 | Welded, roll-top | IPX7 | 1.35 kg | None | Immersion risk, buoyancy |
| SL-C811 | Welded, waterproof zip | IPX6 | 2.6 kg | 20–25 mm | Protection plus load carriage |
The SL-C811 is the only case in the range that combines a welded waterproof shell with full padding and exterior load carriage. It is also the heaviest, and that is the trade a buyer is making.
Precision and tactical rifle transport where the firearm carries an optic and suppressor; agency and unit equipment programmes requiring MOLLE compatibility and identification panels; vehicle-based operations where a case is loaded and unloaded repeatedly in weather; competition shooting where a rifle travels with accessories attached to the exterior; guided operations transporting client rifles across rough ground; and any programme where a firearm must arrive both dry and undamaged rather than one or the other.
| Item | Specification |
| Individual packing | PE protective bag |
| Carton | 135 × 38 × 38 cm |
| Units per carton | 4 pcs |
| Carton gross weight | approx. 11.5 kg |
| Volume per unit | approx. 0.049 m³ |
| 20 GP loading | approx. 570 pcs |
| 40 HQ loading | approx. 1,390 pcs |
| MOQ | 300 pcs |
| Sample lead time | 7–10 days |
| Production lead time | 30–45 days |
| Trade terms | EXW / FOB / CIF |
| Certifications | ISO 9001, BSCI, SMETA, GRS (material dependent) |
Container figures are calculated from carton volume and are indicative; final loading is confirmed against the packing list at booking.
| Included Item | Quantity |
| Tactical Waterproof Rifle Case (SL-C811) | 1 |
| Backpack straps | 1 set |
| Detachable shoulder strap | 1 |
| PE protective bag | 1 |
• 12-month warranty against manufacturing defects, including welded seams and retention hardware
• Replacement retention straps and buckles supplied for dealer service programmes
• Welding parameter records retained per project for OEM quality files
• Reference firearm fit consultation for retention strap positioning
• Third-party inspection by SGS or QIMA arranged on request
Competitors were transporting scoped rifles with suppressors fitted, which ran out of length in the 122 cm cases they had been using. We supplied the 132 cm body and repositioned the retention straps against a reference rifle so the fore-end, receiver, and stock were each secured with the suppressor in place. 350 pcs, 44 days.
The requirement was MOLLE compatibility on a waterproof case, and the buyer had previously been offered stitched webbing on a welded shell. We supplied the laser-cut panel specification with jet test results taken on a finished unit with the panel fitted, plus a hook-and-loop panel sized for unit identification. 500 pcs, 45 days.
Client rifles were being loaded and unloaded from vehicles in weather several times a day, and the operation wanted one case that would keep guns both dry and unmarked. The combination of welded shell and retention system addressed both, and the backpack harness handled the walk-in sections. 400 pcs, 43 days.
“Suppressor on, scope on, and it still closed with clearance. That was the whole specification for us.”
— Team Manager, Precision Rifle Programme
“Everyone else offered us stitched MOLLE on a welded case and called it waterproof. You laser-cut it and had the test to back it.”
— Procurement Officer, Agency Programme
“The retention straps are what stopped the wear. The rifles used to come out marked from travelling inside the case.”
— Operations Manager, Guiding Operation
At 132 cm external it suits rifles up to roughly 120 cm overall, which covers scoped precision rifles with suppressors fitted. Measure the firearm as it will be cased — optic, suppressor, and bipod attached — and allow clearance beyond that figure. 122 cm and 140 cm bodies are also quoted.
IPX6 under IEC 60529 — protection against powerful water jets from any direction, covering heavy rain, deck wash, and hose-down. It is not immersion rated. Customers whose cases may go fully underwater should use our welded roll-top range, which is immersion rated and floats.
The grid is laser-cut into a welded outer panel rather than sewn as webbing rows. There is no stitching, and the panel itself is welded to the shell, so the waterproof barrier behind it stays continuous. Stitched MOLLE on a welded case puts a perforation at every bar-tack.
Padding absorbs an impact that reaches the firearm. Retention stops the firearm moving in the first place, which is the mechanism that produces contact wear over long journeys. Six to eight adjustable points secure the fore-end, receiver, and stock separately.
An egg-crate profile compresses progressively rather than all at once, and its raised sections press down onto the firearm to hold it against the base. The gun is held between two foam surfaces rather than resting loose under a lid.
Because the loads differ. The base takes ground contact and drop energy at 15 mm, the lid does the retention work at 20–25 mm, and the sides need 10 mm to stop edge contact without adding bulk to a 10 cm profile.
Because it does more. Welded waterproofing, 20–25 mm of layered padding, a retention system, MOLLE, and a backpack harness together come to approximately 2.6 kg against 1.1–1.35 kg for an unpadded welded case. It should be specified where the protection and load carriage are needed.
Opening from the muzzle end alone gives access to the barrel section without exposing the whole interior, which is useful working from a vehicle or a prone position. On a 132 cm case that matters more than on a short one.
Yes, and we recommend setting them against a reference firearm at sampling so each strap lands at the fore-end, receiver, and stock of the intended rifle rather than at generic positions.
It is specified as a single-rifle case with room for accessories. Two-rifle configurations can be quoted with revised retention layout and increased thickness — confirm the requirement at the development stage.
A welded logo patch, printing, and the hook-and-loop panel, which accepts identification or unit patches without additional attachment to the barrier. Embroidery is not recommended on a waterproof shell.
MOQ 300 pcs, samples in 7–10 days, production in 30–45 days, quoted EXW, FOB, or CIF. OEM and ODM development covers length, foam grade and thickness, retention layout, MOLLE panel design, colour, branding, and packaging.
Address
No. 88, Fenggang Section of Dongshen Road, Fenggang Town, Dongguan City, Guangdong Province, China
Tel